Oct 28, 2026Chain Operations
Footring Design: The Tableware Specification Nobody Reads
The footring carries the plate's whole weight and grinds its stack-mates for years — yet appears on almost no spec sheet. Foot height, glazing and diameter: the quiet spec that decides fleet life.

Footring Design: The Tableware Specification Nobody Reads
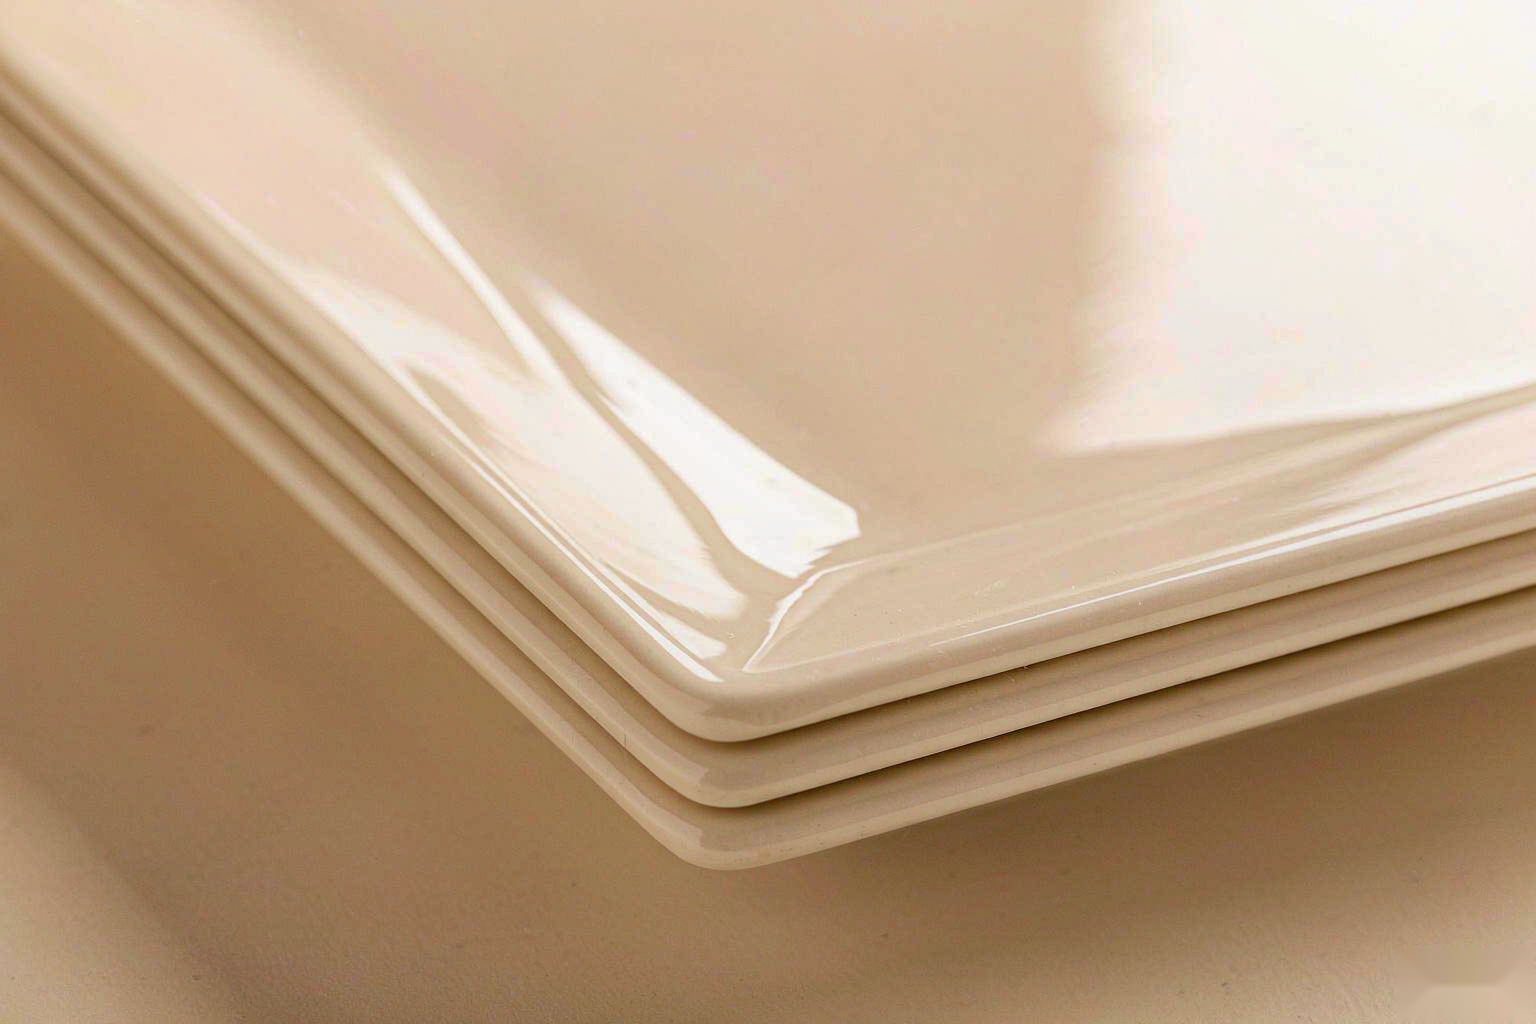
Turn a dinner plate over. The unglazed or glazed ring on the bottom — the part that never faces a guest, never appears in a menu photo, and gets one line (if any) on most specification sheets — is carrying the entire fleet right now. It carries the plate on the table, the stack on the shelf, and the rack's vibration through the wash. And it has been grinding quietly against the rim of the plate below it since the day the shipment arrived.
Footring design is the most consequential invisible specification in commercial tableware. Chains that specify it retire fleets on schedule; chains that don't retire them on evidence — chips and scratches appearing on the storage side of plates, a pattern no amount of careful service prevents. This guide reads the footring the way a supplier's production engineer does.
What the Footring Actually Does
Three jobs, all structural:
Load bearing. The foot is the only contact point with the table. Its diameter against the plate's overall width sets the stability envelope — a narrow foot on a wide, heavy plate rocks; a foot too wide defeats the raised design that makes one-hand pickup possible.
Stack separation. In a stack, the foot of the upper plate rests on the food surface or rim of the lower plate. What it does there — glide, grind or chip — is a materials question decided by the footring's finish.
Lift geometry. On bowls and Asian formats especially, foot height creates the finger clearance that lets staff lift a hot bowl one-handed. The traditional high foot of Japanese vessels is ergonomics, not style.
The Three Design Variables
Foot height. Measured from the table to the plate's underside. Low feet stack compactly and read contemporary; high feet lift for finger clearance, present the plate with more presence, and — on bowls — keep hot contents off the table surface. Asian-format programs specify foot height deliberately; Western programs discover it when a new bowl format arrives that servers cannot lift cleanly.
Foot diameter. The stability variable. The working rule from production engineering: wider plates need proportionally wider feet. A wide-rimmed format with a narrow foot passes the showroom table and fails the wobble test on a real table with a real knife resting on the edge. At sampling, the wobble test is mandatory: plate on flat surface, press each edge, feel for rock.
Foot finish. The variable that decides stack-mate fate. Options in production:
Finish | Grip on stack-mates | Marks left on plate below | Best for |
|---|---|---|---|
Fully glazed, polished | Minimal | Negligible | All chain programs |
Glazed, unpolished | Low | Light scuffing over time | Acceptable second tier |
Unglazed, sanded | Moderate | Grinding, micro-chips at rim | Avoid for stacked fleets |
Unglazed, rough | High | Visible damage within months | Disqualifying |
The finish column is why two visually identical plates can age completely differently. The grinding mechanism is simple: unglazed ceramic against glazed ceramic, loaded with weight, vibrated in a dish rack, is a lapidary setup. The plate below is being polished — destructively — at its most vulnerable point, the rim.
The Stack Test: Five Minutes That Predict Years
The verification protocol that belongs in every receiving bay and every first-article review:
1. The slide test. Stack eight to ten samples. Slide the stack gently across a smooth table, twice. Inspect the lower plates' rims under raking light. Any scuffing or micro-chipping from a gentle slide will compound through thousands of rack cycles — reject the batch. 2. The wobble test. Each sample on a flat surface, press opposite edges. Any rocking foot fails the piece for guest-facing service. 3. The finger test. Run a finger around each footring. Roughness you can feel is roughness that works on stack-mates. 4. The tape test (optional but decisive). Press low-tack painter's tape around a footring, remove, and inspect the tape — it collects the grit an unglazed foot sheds.
Chains that adopt the slide test into standard receiving stop storage-side damage before it starts — and give their suppliers a specification to hold, because the feedback travels back up the chain.
Footring and the Dish Room
The foot's third life happens in the wash. Footring interiors trap food soil and are the hardest zone to clean on any plate — foot design determines whether the spray can reach. Deep, narrow foot wells hold debris and wash water; shallow, open feet release both. In high-volume operations this shows up as spot-frequency on the foot zone at inspection — a dish-room pattern with a tableware-design root cause.
Racking multiplies it: plates standing in racks put footrings against rack pins and adjacent rims. Polished glazed feet survive racks; rough feet damage the neighbors they touch. The full rim-and-foot pairing is covered in our rim profile guide — the two specifications are one system.
Writing the Specification
The line items that make a footring real on paper:
Foot height in millimeters, per format class (plates, bowls, Asian formats)
Foot finish: "fully glazed and polished" — the phrase that matters
Stability requirement: passes wobble test on flat surface
Stack behavior: passes gentle slide test without marking stack-mates
Suppliers respond to these lines because they are production-checkable. A footring specified this way costs nothing extra to make correctly — the expense is only in re-doing fleets that were never specified at all.
Frequently Asked Questions
Why do expensive plates sometimes have unglazed feet? Fine-dining porcelain traditions kept unglazed feet for authenticity — in low-stack, hand-washed service. Translated into a dish-rack chain fleet, the same foot becomes a grinding tool. Context defines the spec.
Can unglazed feet be polished after purchase? Some operators hand-polish feet with silicon-carbide paper. It reduces grinding but never matches a glazed, polished production finish — and it is labor forever. Specify correctly instead.
Do melamine pieces have this problem? Melamine feet are molded and typically smooth, so grinding is minimal — the format's foot issues are warp-related seating instead. The stack test still catches both materials' bad actors.
How high should a bowl foot be? Tall enough for one-hand finger pickup with a full bowl — practically, verify by hand at sampling with a real portion weight. Asian-format bowls carry higher feet for exactly this lift.
What is the fastest fleet audit for foot damage? Pull twenty random plates from service. Inspect rims under raking light for crescent scuffs and micro-chips on one side — the signature of footring grinding in storage. Find it, and the specification gap is already costing money.